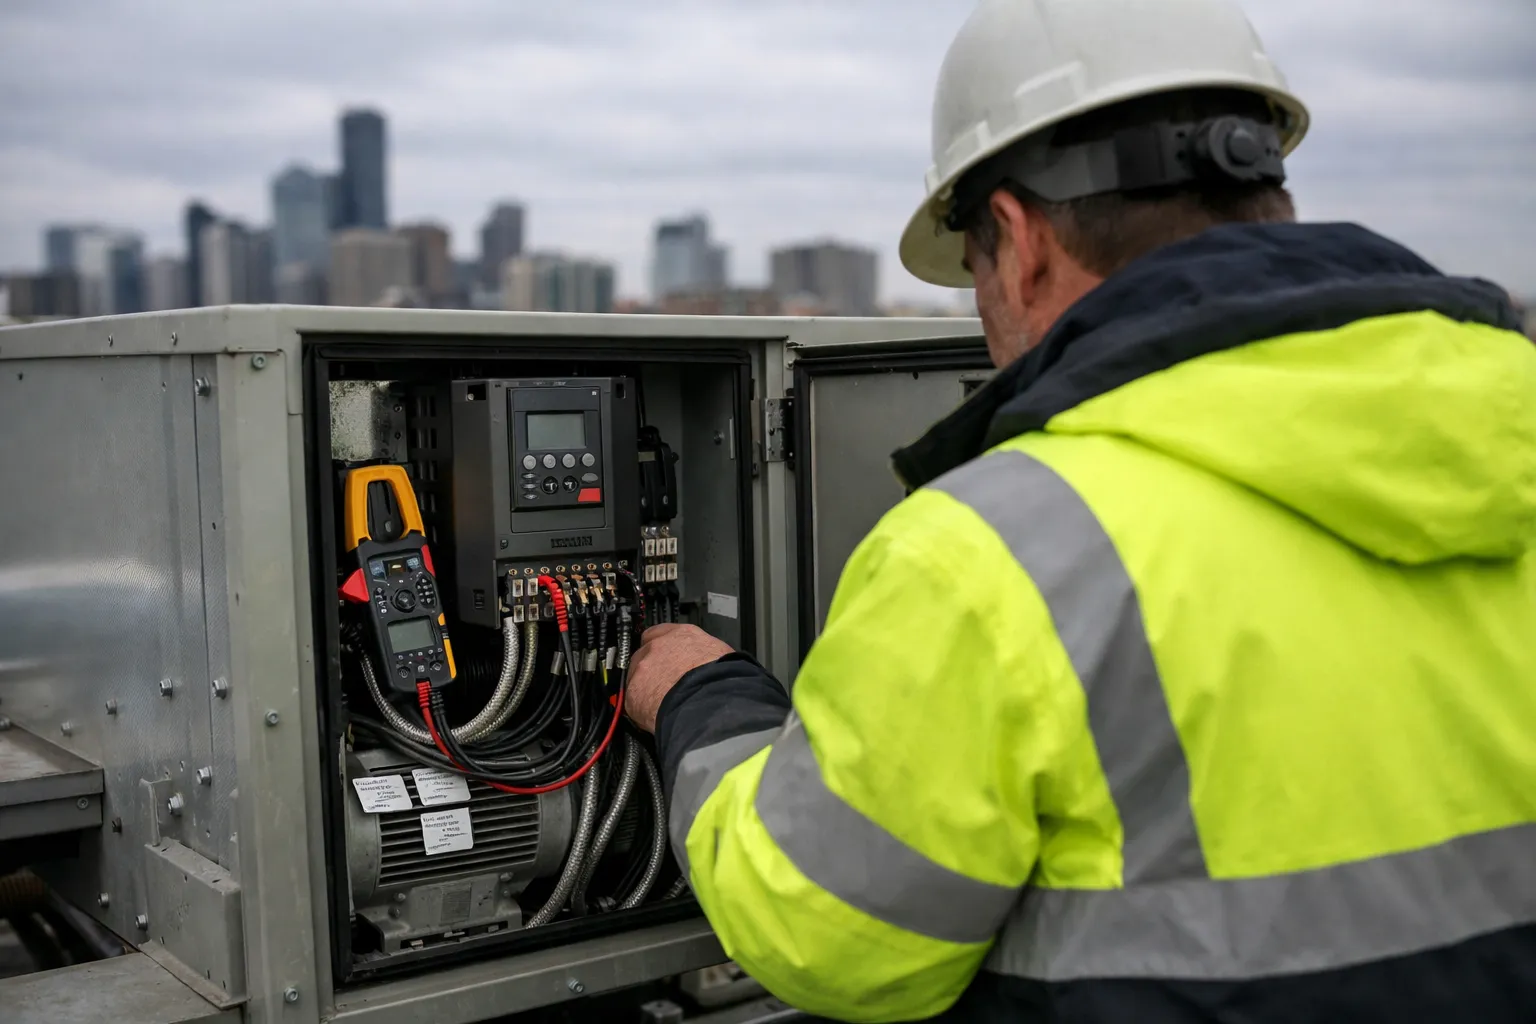
Upgrading rooftop units (RTUs) with variable‑speed fans via variable frequency drives (VFDs) is one of the highest‑value retrofits for technicians, facility managers, and HVAC hobbyists. When done correctly it cuts fan energy dramatically, improves tenant comfort and IAQ control, reduces noise, and enables demand‑driven ventilation and advanced controls. This guide walks through a practical, field‑ready process: site assessment, VFD and electrical selection, mechanical prep, control integration, commissioning and testing, power‑quality checks, and maintenance considerations.
Why retrofit RTU fans with VFDs?
- Energy savings: Fan power follows the affinity law—power varies roughly with the cube of speed—so modest speed reductions yield big energy reductions.
- IAQ and ventilation control: Variable fans make CO2‑based demand ventilation, enthalpy recovery integration, and economizer staging smoother and more accurate.
- Noise and comfort: Reduced motor speed lowers tonal noise and allows smoother airflow transitions.
- Extended equipment life: Soft starting reduces inrush current and mechanical stress; balanced operation reduces belt and bearing wear.
When to consider a retrofit
- RTUs with constant‑speed motors (belt or direct‑drive) that run long hours or serve spaces with variable occupancy.
- Motors in the 1–15 HP range—common in small to mid‑size commercial RTUs—where VFD economics are favorable.
- Systems that could benefit from demand control ventilation, tighter pressurization, or quieter operation.
- Units with motors in good mechanical condition: bearings, shafts, pulleys, and belts should be serviceable; VFDs hide but don’t solve mechanical faults.
Pre‑retrofit assessment (Do this first)
- Document the RTU: manufacturer, model, motor nameplate (HP, voltage, phase, full‑load amps), fan type (centrifugal/axial), and existing controls.
- Measure baseline: supply CFM (pitot, balometer, or anemometer), static pressures (inlet and discharge), filter pressure drop, ambient and entering air temps, and run hours (use BAS logs if available).
- Inspect mechanicals: belt condition, pulley alignment, bearing play, shaft runout; plan to repair/replace before VFD install.
- Identify control interfaces: Does the RTU have BACnet/MODBUS, analog I/O, or simple dry contacts? Plan how the VFD will receive speed setpoints and send status.
- Check electrical capacity: available breaker space, service voltage, neutral and ground conditions, and upstream transformer capacity.
Selecting the VFD and accessories
Key selection points:
- Rated horsepower: pick a VFD rated at or above the motor HP. For continuous duty fans, choose a VFD with 110–125% overload capacity depending on the application.
- Voltage and phase: match the motor (e.g., 230/460 V, 3‑phase). For single‑phase supply to three‑phase motors, use appropriate phase converters—prefer three‑phase supply where possible.
- Control mode: Volts‑per‑Hz is fine for many fans; sensorless/vector control gives better low‑speed torque and more accurate RPM control if needed.
- Communications: BACnet MS/TP or IP, Modbus RTU/TCP, and standard 0–10 V or 4–20 mA analog I/O options are useful for BAS integration.
- Enclosure rating: NEMA 1 for indoor units, NEMA 3R outdoors or inside rooftop curbs; consider external VFD cabinets if rooftop exposure or greasy environments are present.
- Harmonic mitigation: for installations with multiple VFDs or sensitive upstream equipment, include line reactors (5–7% impedance), passive harmonic filters, or consider a 12‑pulse drive solution.
- EMC/grounding: select units with proper EMC filters and follow cable shielding and grounding guidelines to avoid motor bearing currents and BAS noise.
Mechanical preparation and motor considerations
- Repair or replace worn bearings and pulleys. VFDs reduce torque spikes but don’t tolerate a failing bearing.
- For belt drives, document pulley ratios and consider converting to direct‑drive if long‑term maintenance is a concern. If keeping belt drive, ensure correct belt tension at full and minimum speed.
- Verify motor insulation class (B/F) and service factor. Older motors with marginal insulation may overheat at reduced cooling speeds—confirm allowable ambient and continuous operating points.
- Install shaft grounding brushes or insulated bearings if bearing currents are a concern for long cable runs.
Electrical installation: practical tips
- Follow LOTO and local code. De‑energize and verify zero voltage on motor leads before starting work.
- Mount a fused disconnect or fused motor controller upstream of the VFD for maintenance isolation.
- Keep motor cable runs short where possible (50 m preferred); use shielded motor cable, bonded at the VFD end per manufacturer guidance.
- Install a dedicated ground conductor sized per NEC tables and VFD manufacturer specs. Poor grounding causes EMI and controls noise.
- If the RTU lacks an adequate neutral or the VFD requires a phase converter, consult an electrician—avoid ad hoc solutions.
Control integration and strategy
Determine the control objective early: constant static pressure, constant airflow, variable ventilation, or pressure control for stair pressurization.
- Static pressure control: use a downstream static pressure sensor and a PID loop on the VFD. Set the sensor location carefully (in straight duct, away from dampers).
- Constant airflow: use a certified airflow station or pitot array and program a feedback loop. Account for filter loading—use differential pressure across filter to adjust min speed.
- Demand control ventilation: integrate CO2 sensors and BAS signals to set minimum fresh air CFM; use the VFD to ramp to minimum ventilation rather than pulsing dampers.
- Analog vs digital: 0–10 V signals are common but subject to noise—prefer BACnet or modbus when available for robust two‑way control and alarming.
- Set frequency limits: program a minimum frequency that overcomes static pressure and damper forces; set a maximum frequency for motor protection and noise control.
Commissioning: tests and acceptance criteria
Commissioning is where the benefits are realized. Execute and document the tests below.
- Functional power‑up: verify VFD boots, communication with BAS, and that E‑stop, door switches, and safeties are intact.
- Motor identity check: spin the motor at 20–30% speed and verify direction; correct wiring if direction reversed.
- RPM vs frequency verification: measure RPM (tachometer) at several frequencies (e.g., 30%, 50%, 70%, 100%); calculate and confirm proportional behavior.
- Current and temperature checks: log motor current during ramps and steady speeds; compare to nameplate full‑load amps. Monitor motor and VFD case temps during a 1–2 hour soak at typical operating points.
- Airflow and pressure testing: measure CFM and static pressure at baseline and at stepped speeds. Confirm the expected cube‑law power reduction and desired CFM control accuracy.
- Filter differential: measure filter dP and set min speed or a filter alarm point when dP exceeds acceptable limits (typically 0.5–1.0 in. w.c. depending on filter type).
- Power quality: measure supply current waveform and total harmonic distortion (THD) with a power quality analyzer. THD under 5–8% is desirable; if above thresholds, add line reactor or filter.
- Interlock and alarm tests: verify loss‑of‑comm, high‑temp, freeze stat, fire alarm, and manual override behavior.
Estimating savings and payback (practical example)
Use the affinity laws for rough first estimates: P2 ≈ P1 × (RPM2 / RPM1)^3.
Example: a 5 HP motor (5 × 0.746 = 3.73 kW) running full speed draws ~3.7 kW. If average operating speed is reduced to 70% to match ventilation needs, motor power ≈ 3.73 × 0.7^3 ≈ 1.27 kW. Energy saved ≈ 2.46 kW while reduced speed applies. Multiply by operating hours and local energy cost to estimate annual savings. Factor in VFD cost, line reactor, and labor to calculate payback—typical paybacks for medium‑to‑long‑running RTUs range from 1.5 to 4 years depending on run hours and electricity rates.
Common problems and troubleshooting
- Motor overheating at low speed: verify motor cooling, ensure minimum speed is high enough for motor cooling or install a separately powered cooling fan.
- VFD tripping on overcurrent during startup: check accel/decel times and torque requirements; lengthen acceleration and verify no mechanical binding.
- BAS communication noise: ensure shielded comms cables, correct grounding, and proper EMC filter installations.
- Excessive harmonics affecting nearby equipment: add a line reactor or passive harmonic filter, or place VFD on dedicated feeder.
- Pulsing airflow or hunting: tune PID gains for static pressure/flow loops, add a small integral term, and set minimum ramp rates to avoid oscillation.
Maintenance and lifecycle tips
- Log VFD alarms, firmware versions, and runtime hours; review monthly for abnormal trends.
- Keep VFD ventilation clear and replace cooling filters. Periodic internal dust removal by a qualified technician prevents overheating.
- Retension belts and inspect bearings at regular intervals—VFDs reduce but do not eliminate mechanical wear.
- Keep a spare VFD (or critical spare components like power modules) on site for mission‑critical systems to minimize downtime.
Checklist before you leave the site
- Baseline and post‑retrofit data logged: RPM, current, CFM, static pressures, filter dP, and THD readings.
- Control setpoints documented: min/max frequency, PID gains, sensor locations, and alarm thresholds.
- Wiring labels and updated single‑line diagram for facility records.
- Operator training: basic VFD status reading, local override procedure, and emergency stop locations.
- Maintenance schedule and warranty paperwork handed to facility staff.
Conclusion
Retrofitting RTUs with variable‑speed fans is a practical retrofit with measurable outcomes: energy reduction, improved ventilation control and IAQ, and quieter operation. Success hinges on thorough pre‑assessment, correct VFD and accessory selection, sound mechanical repairs, careful electrical work, robust control integration, and commissioning with power‑quality checks. For HVAC enthusiasts and pros, following this step‑by‑step process reduces surprises in the field and maximizes the chances of a smooth, high‑return retrofit.